Hey folks, if you’ve ever worked with planetary gear parts—whether you’re a maintenance tech, design engineer, or someone who’s just spent hours troubleshooting a misfitting gear set—you know how one tiny measurement slip-up can derail an entire build. As a planetary gear parts supplier, I’ve spent thousands of hours in our QC lab measuring every single component that leaves our warehouse, and let me tell you: it’s not just about grabbing a caliper and calling it a day. It’s about knowing exactly which dimensions matter, how to measure them right, and what mistakes to avoid so you don’t end up with parts that don’t mesh, grind, or flat-out fail. Planetary Gear Parts
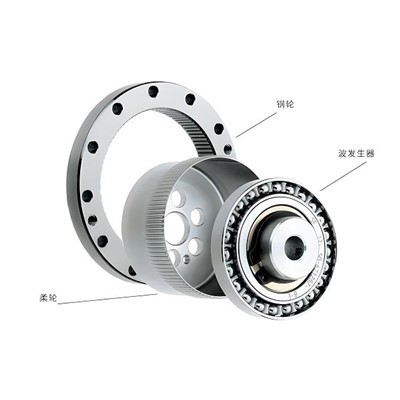
First off, let’s cut through the jargon for a sec—planetary gears are that set of gears with a central sun gear, a ring gear on the outside, and little planet gears spinning in between, right? Each of these parts has critical specs, and if you get even one wrong, the whole system is toast. The biggest mistake I see people make is mixing up “critical dimensions” with “all dimensions”—you don’t need to measure every tiny edge of a planet gear, just the ones that affect fit, mesh, and load. Let’s break it down part by part, because measuring a sun gear is way different than measuring a ring gear.
Starting with the star of the show (literally): the sun gear. This tiny central gear is what transfers power into the planetary set, so its dimensions have to be spot-on. First up, pitch diameter—this is the circle where the teeth effectively mesh with other gears, not the actual outer diameter of the gear teeth. A lot of new guys use an outside caliper to measure from tooth tip to tooth tip, but that’s wrong. You have to calculate pitch diameter using the number of teeth and the module (or diametral pitch, depending on if you’re using metric or imperial) of the gear. Wait, let’s keep that simple: module is metric, so if you have a sun gear with module 2 and 20 teeth, pitch diameter is 40mm. But how do you measure that if you don’t want to do math? You can use a gear tooth micrometer—this little tool sits on the face of two teeth and measures the distance between them, which you can plug into a formula to get pitch diameter. Way more accurate than a regular caliper. Also, don’t skip the tooth thickness—if the sun gear’s teeth are too thin, they’ll wear out fast; too thick, and they won’t fit between the planet gears. I always tell our customers: if you’re measuring tooth thickness, use a involute gear tooth caliper, not a standard one. We’ve had a client send back a batch because someone used a regular caliper and thought the teeth were fine, but the involute caliper showed they were 0.02mm too thin—enough to cause noise and early failure.
Next, the planet gears—these are the ones that spin around the sun gear, so they have to mesh perfectly with both the sun and the ring gear. The big ones here are pitch diameter (same as sun gear, but for planets), bore diameter, and tooth runout. Bore diameter is non-negotiable because that’s where the planet shaft goes. If the bore is even a hair too small, you can’t press the shaft in; too big, the planet will wobble and cause vibration. We use coordinate measuring machines (CMM) for high-volume orders, but for smaller runs or field checks, a dial bore gauge works way better than a vernier caliper. Vernier calipers can be wobbly if you’re holding them by hand, but a dial bore gauge locks into the bore and gives you a precise reading—we’re talking thousandths of a millimeter here, which is the difference between a smooth-running gear and a noisy one. Also, tooth profile runout: that’s how straight the teeth are around the gear. If a planet gear is slightly oval, it’ll grind against the sun and ring, leading to heat and breakdown. To measure runout, mount the gear on a precision arbor, spin it, and use a dial indicator to check the total variation around the teeth. It sounds like overkill, but I’ve seen a robotic arm fail because a planet gear had 0.05mm of runout—small enough that no one noticed at first, but after 100,000 cycles, it seized up.
Then there’s the ring gear, the outer circular gear that all the planet gears mesh with. This is the trickiest one to measure, because it’s internal teeth—you can’t just stick a caliper inside and measure. The main dimension here is internal pitch diameter. How do you do that? First, you can use an internal gear tooth caliper, which reaches inside the ring gear and measures the distance between two internal teeth. Or, for more accuracy, we use a small-hole gauge and then measure the distance between the holes with a micrometer, then adjust for the tooth thickness. Another thing people miss with ring gears is the face runout—how flat the gear’s mating surface is. If the ring gear is warped even a little, when it’s bolted to a housing, it’ll tilt, and all the planet gears will mesh unevenly. We check face runout with a surface plate and a dial indicator: set the ring gear flat on the plate, drag the indicator across the face, and any variation over 0.03mm is a no-go for us. I once had a customer who tried to machine a ring gear themselves and skipped the face runout check—they ended up with a gear that had 0.1mm of runout, and their entire planetary drive failed in a wind turbine gearbox. Ouch.
Wait, I can’t forget about the center distance. That’s the distance between the sun gear’s center and a planet gear’s center, and it has to be exactly the same for all planets, otherwise they won’t mesh evenly. How do you measure that? If you’re assembling a set, you can use a vernier caliper between the centers of the sun and a planet, but to check it on individual parts, you can use a gear center distance gauge, or if you’re a supplier like us, we use a gear rolling test stand. We roll all three gears (sun, planet, ring) together and measure the backlash—backlash is the tiny gap between the meshing teeth, and it’s directly tied to center distance. Too much backlash, and you get noise and power loss; too little, and the gears bind up. We target a backlash of 0.05mm for most standard planetary sets, and that’s only achievable if all center distances are within 0.02mm of each other. That’s why our QC team does 100% backlash checks on every custom order, not just random samples.
Now, let’s talk about the tools—you don’t need a million fancy machines, but the cheap ones will get you cheap results. I’ve seen guys use a $10 vernier caliper from a hardware store to measure critical gear dimensions, and that’s a mistake. A good digital caliper is fine, but for tooth-specific measurements, you need a gear micrometer or involute caliper. For bores, a dial bore gauge is way more accurate than a vernier, especially for smaller diameters. If you’re doing high-volume work, a CMM is a game-changer—it can measure 10+ dimensions on a single part in seconds, and it’s way more precise than any manual tool. But if you’re in the field, maybe replacing a gear on a construction site, a set of gear calipers and a dial indicator will get you 90% of the way there.
Also, here’s a pro tip that most suppliers won’t tell you: temperature matters. Metal expands when it’s warm, so if you measure a gear right after it’s been machined (when it’s 50°C from cutting), and then install it when it’s 20°C, the dimensions will be off by a tiny amount—enough to cause problems. We always let parts sit at room temperature for 24 hours before measuring, and we note the ambient temp on every QC sheet. It’s a small step, but it’s saved us from so many customer complaints.
Wait, let’s talk about common mistakes we see all the time. First, measuring the wrong teeth. A lot of people use the same tooth to take multiple measurements, but if that tooth has a tiny defect, it skews all the readings. We always measure 3 different teeth around the gear and take the average. Second, not accounting for pressure angle. The pressure angle is the angle of the gear teeth (usually 20° for standard gears), and if you ignore that, your pitch diameter calculation will be wrong. If you’re using a gear caliper, it’s built for the standard pressure angle, so that’s fine, but if you’re doing it manually, don’t skip that. Third, not checking for concentricity. Concentricity is how aligned the gear’s teeth are with its bore—if the teeth are off-center from the bore, even if all other dimensions are perfect, the gear will wobble. We measure concentricity with a CMM, but a rough field check is to mount the gear on a shaft and spin it while looking at the teeth—if they jump at all, concentricity is off.
As a planetary gear parts supplier, this is why we’re so picky about measurements. Our parts go into everything from farm equipment to wind turbines to robotics, and if one measurement is off, it’s not just a bad part—it’s downtime for our customers, which costs them thousands of dollars. That’s why every part that leaves our facility gets a full set of measurements: pitch diameter for sun, planet, and ring gears; bore diameter and concentricity for planets; face runout for ring gears; center distance; and backlash. We send that QC report with every order, so our customers don’t have to guess if the parts will fit.
If you’re someone who needs planetary gear parts, whether you’re building a new system or replacing worn ones, don’t cut corners on measuring. Even if you’re not ordering from us, take the time to learn which dimensions are critical for your specific application. For example, a robotics planetary drive needs tighter backlash than a construction tractor, so your measurements need to be more precise. If you’re not sure what specs you need, just reach out—we’ve helped hundreds of customers work through their measurement needs, from small hobbyists to big industrial firms.

At the end of the day, measuring planetary gear parts isn’t rocket science, but it’s a mix of knowing the right specs, using the right tools, and avoiding the small mistakes that add up to big problems. If you’re tired of dealing with ill-fitting gear parts, or you need high-quality, precisely measured planetary components for your next project, don’t hesitate to get in touch with us to discuss your requirements. We’re here to make sure your gears fit, mesh, and perform exactly as they should—no guesswork, no bad parts, no downtime.
Robot Reducer Components References:
- ISO 14540:2017, Mechanical vibration – Vibration of rotating shafts and associated machinery – General requirements for evaluation of vibration severity
- Gear Technology Magazine, "A Practical Guide to Measuring Gear Dimensions for Industrial Applications", 2022
- American Gear Manufacturers Association (AGMA) Standard 2000-A88, Fundamental Gear Quality Standards
Jiangsu Zhengfang Dynamics Technology Co., Ltd.
As one of the most professional planetary gear parts manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy customized planetary gear parts made in China here from our factory. Contact us for pricelist.
Address: Building 3, No. 69 Feitian Avenue, Jiangning District, Nanjing City, Jiangsu Province
E-mail: hanks.liu@zfdynamics.com
WebSite: https://www.zhengfangdongli.com/
