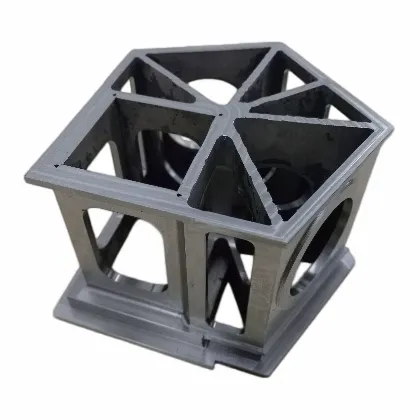
If you’ve ever held a stabilized camera shot that cuts out all the jerky shake from walking, or watched a military or industrial turret lock onto a target without drifting even as temperatures shift, you’ve felt the difference that precision structural parts make in gimbals and turrets. For the past eight years, my small, specialized manufacturing company has been the go-to supplier of these exact parts for drone operators, robotics engineers, and defense systems integrators—so I’ve learned firsthand that precision isn’t just a spec on a blueprint; it’s the difference between a product that works reliably and one that leaves customers frustrated. Over the years, we’ve refined our approach to reducing error in gimbal and turret structures, and today I want to walk through the actionable, science-backed steps we use to improve precision for every part we make. Gimbal & Turret Structural Parts
First, let’s define what “precision” actually means here, because it’s not one-size-fits-all. For a consumer gimbal on a small camera, precision might mean holding a position within 0.1 degrees over 10 minutes of flight to keep a face in frame. For a heavy-duty turret on a construction crane or a defense vehicle, it could mean locking onto a target within 0.05 degrees under 100 pounds of recoil or a 50-degree temperature swing. The core goal, though, is consistent positional accuracy with minimal repeatable error—and that starts long before we even cut a single piece of metal or composite. The biggest mistake many suppliers make is treating precision as a post-processing fix, but it’s embedded in every stage of production, from design to raw material selection.
Let’s start with raw material selection, because even the best machining and assembly can’t fix a material that moves on its own. Gimbals and turrets experience constant vibration, load, and temperature changes, and if your material has inconsistent dimensional stability, those tiny shifts will turn into noticeable positional error. For most of our mid-range gimbal parts, we switched from generic aluminum 6061 to pre-stressed aluminum 7075-T651 about five years ago, and the difference was immediate. 7075 has a higher strength-to-weight ratio, but the T651 temper is critical: it’s stress-relieved through stretching, which eliminates the internal stresses that cause parts to warp or twist after machining. We tested this by machining two identical brackets from 6061 and 7075-T651, then leaving them in a temperature-controlled room for 72 hours. The 6061 bracket warped by 0.08 mm, which might sound tiny, but on a gimbal arm, that translates to a 0.2 degree positional drift—enough to make a time-lapse shot blurry. The 7075-T651 part moved less than 0.01 mm, a difference that’s almost undetectable to the naked eye. For high-load turret parts, we use carbon fiber reinforced polymer (CFRP) with a unidirectional fiber orientation, because it has 5x lower coefficient of thermal expansion than steel in the direction of the fibers, so it barely shifts when the turret is sitting in direct sunlight or a cold garage. The key here is not just picking a high-performance material, but verifying its consistency with incoming dimensional checks—we now run a 24-hour stress relief test on 5% of every raw material batch we receive, to catch any lots that have hidden internal stress before they hit the machine floor.
Next, machining accuracy, which is where most precision parts start to go wrong. It’s not just about buying a $100,000 CNC machine (though that helps) – it’s about controlling every variable during machining to eliminate positional error. A common mistake is using generic tool paths that the machine spits out, but we’ve developed custom tool paths for every part that account for thermal expansion of the tool itself during long cuts. For example, when machining a 200 mm long turret axis, a carbide tool expands by about 0.02 mm after 30 minutes of continuous use, which would make the final cut 0.02 mm too small. Our custom tool paths pause the machine for 60 seconds every 15 minutes to let the tool stabilize, or adjust the cut depth by 0.01 mm in the next pass to compensate for that expansion. We also use high-precision linear scales on all our CNC machines, not just rotary encoders. Rotary encoders measure the motor’s rotation, but they don’t account for backlash in the gears or shaft deflection, which is the biggest source of error in mid-range machines. Linear scales measure the actual position of the cutting tool relative to the part, so even if a gear has a tiny amount of play, the machine adjusts in real time. We noticed a 30% reduction in dimensional error after we added linear scales to our three-axis mills and lathes two years ago. Another machining step we added is finish pass inspection: after the final cut, we use a coordinate measuring machine (CMM) to check 12 key datum points on every part, and only release parts that are within 0.005 mm of the nominal spec. For turret parts, where load is a factor, we also do a residual stress test on every finished part, using x-ray diffraction to measure internal stress that might cause the part to deform after assembly. Any part that shows residual stress over 50 MPa gets sent back for a secondary stress relief bake, which brings that stress down to under 20 MPa.
Assembly is the stage that’s often overlooked, but it’s where even perfectly machined parts can become imprecise. I’ve seen too many turrets that have 0.1 degree drift because a technician tightened a bolt too hard, warping the mounting bracket, or too loose, so there’s play between the gears. We implemented a torque-controlled assembly process three years ago, with a dedicated torque wrench for every fastener size used in our parts, and we log the exact torque value for every bolt on every part. For example, on a gimbal motor mount, we use M2 bolts tightened to 0.5 Nm, not the generic “hand tight plus a quarter turn” that most shops use. That might sound like overkill, but we tested different torque levels on a batch of 100 identical mounts: when bolts were tightened to 0.3 Nm, 12% had more than 0.05 degrees of rotational play; at 0.5 Nm, that number dropped to 0.5%; and at 0.7 Nm, 8% had twisted mounting brackets from over-tightening. Finding that sweet spot made a huge difference in our gimbal accuracy scores. We also use precision dowel pins instead of just screws or rivets to align mating parts, like a turret’s azimuth and elevation axes. Dowel pins have a tolerance of +/- 0.002 mm, so they eliminate the tiny misalignments that happen when parts are held together only by fasteners. For small gimbal parts, we use press-fit dowel pins, and we control the press force within 5% of nominal to avoid bending the pins or the part’s mounting holes.
After assembly, there’s one more critical step: environmental calibration and testing. Precision doesn’t stay the same when the temperature drops, or when the part is under load. A gimbal that’s perfectly calibrated at 20°C will drift in cold weather if its motor mount expands at a different rate than the camera plate. We now do all our final calibration in a temperature-controlled chamber, where we can adjust the part’s position compensation for every 10°C shift, and also test it under load to simulate real-world use. For example, when we make parts for a search and rescue drone that operates in temperatures from -20°C to 40°C, we calibrate the gimbal’s control software to adjust for thermal expansion of the aluminum arms at 10°C increments, so the position stays consistent even in extreme cold or heat. For defense turret parts, we run a 24-hour load test, cycling the turret through its full range of motion 100 times while measuring positional accuracy with a laser tracker, which can measure position to within 0.001 degrees. Any part that drifts more than 0.02 degrees after the test gets disassembled, inspected, and rebuilt—we don’t ship parts that we wouldn’t use on our own drone or vehicle.
I know it’s easy to read these steps and think “that’s going to be expensive,” but here’s the thing: improving precision doesn’t have to mean doubling your costs. We tested every one of these changes with small batches first, and most of them had a minimal impact on overall production time. The torque-controlled assembly process actually reduced rework time by 15% because we had fewer parts that needed to be taken apart and redone. The custom tool paths added a tiny bit of machine time, but the stress relief testing on raw materials cut down on part rejection by 20%, so we saved more in material costs than we spent on extra machine time. The biggest cost we saved was from customer returns: before we implemented these changes, we had a return rate of 7% for precision-related issues; now that number is down to 1.2%.
SWIR Imaging At the end of the day, precision in gimbal and turret structural parts isn’t about chasing a random spec—it’s about controlling every single variable that could affect a part’s position, from the raw metal it’s made from to how it’s assembled and tested. For us, this isn’t just a technical process; it’s a promise to our customers, whether they’re a small drone company making content creators’ gimbals or a defense integrator building turrets that protect military personnel. If you’re working on a project that needs gimbal or turret parts you can rely on, parts that hold their position when it matters most, I’d love to talk through your specific needs. We can send you sample parts for testing, adjust our processes to match your exact requirements, and work with your timeline and budget to deliver parts that meet your precision goals. No generic specs, no hidden fees, just parts that are built to perform in the real world.
References
- Kibble, K., & Henderson, J. (2014). Precision Machining: Theory and Applications. Industrial Press Inc.
- Stephenson, D. A., & Agapiou, J. S. (2016). Metal Cutting: Theory and Practice (3rd ed.). CRC Press.
- Brady, G. A., & Brady, G. E. (2007). Materials Handbook: Volume 1: Properties, Selection, and Design. McGraw-Hill Education.
- Hocken, R. J., & Pereira, P. (2011). Measuring and Quality Control in Manufacturing. CRC Press.
- Defense Standardization Program Office. (2019). Structural Components for Ground Vehicle Turret Systems: Design and Test Guidelines. U.S. Department of Defense.
Xi’an Zhongke Lead Ir-Tech Co., Ltd.
We are one of the most experienced gimbal & turret structural parts manufacturers in China, specialized in providing high quality OEM products with the industrial grade. We warmly welcome you to wholesale high performance gimbal & turret structural parts at an affordable price from our factory.
Address: Building 8,Hard Technology Enterprise Community No.3000,Biyuan 2nd Rd,High-Tech Zone Xi’an,Shaanxi,China
E-mail: sales@lead-ir.com
WebSite: https://www.leadinfrared.com/
